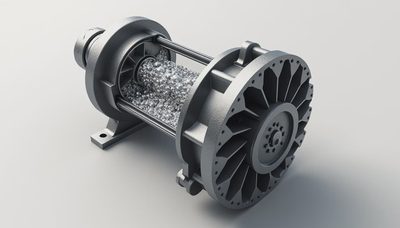
A shovel went quiet on a copper site outside Calama, Chile, with the bucket hanging half full and the operator still in the cab. The hydraulic pump had not failed all at once. It had been whining for weeks, running hot, and losing cycle speed. Nobody stopped the machine. This hydraulic pump failure analysis showed a plugged suction strainer, air entering through a damaged seal, and a pump that had already destroyed its rotating group. I've seen this go wrong. Here's how you avoid it.
Start with Symptoms, Not Parts
Good hydraulic pump failure analysis begins with what the machine was doing before the failure. Ask the operator when the noise started, whether the oil temperature climbed, and if the machine slowed under load. A pump that whines during cold startup may be drawing air or fighting restricted suction. A pump that becomes noisy after warm-up may have worn internal components, low inlet pressure, or oil that is too thin for the operating temperature.
Do not confuse a weak hydraulic function with a bad pump automatically. A plugged return filter, stuck compensator, worn control valve, leaking cylinder, or incorrect relief-valve setting can produce similar symptoms. On an excavator, compare boom, stick, bucket, swing, and travel functions. If every circuit is slow and weak, investigate supply pressure and pump control. If one function is poor, the pump may be innocent.
Field Lesson: On a large wheel loader in Western Australia, the crew changed the main pump twice because the bucket would not lift rated loads. The real problem was a relief valve packed with metallic debris from an earlier component failure. The replacement pumps were damaged by the same contamination.
Check Oil, Filters, and Suction Conditions
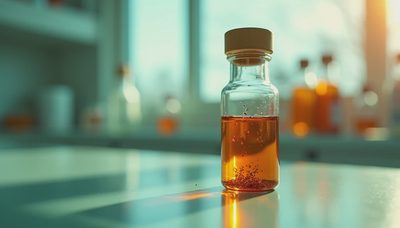
The oil tells a story, but only if you look at it properly. Drain a clean sample into a clear container and inspect it under strong light. Silver glitter suggests wear from steel components. Brass or bronze particles can point toward bearings, bushings, or thrust plates. Milky oil indicates water contamination, while foam often means air is entering the circuit. A burnt odor and darkened oil support an overheating problem, but color alone is not a diagnosis.
During hydraulic pump failure analysis, cut open the old filter rather than throwing it in the waste bin. Spread the media on clean paper and look for particle shape and quantity. A few dull, nonmagnetic flakes mean something different from sharp steel needles. Use the correct filter rating and replace a damaged suction strainer. A restriction on the inlet side can create cavitation, where vapor bubbles form and collapse inside the pump. That collapse pits metal surfaces and produces the familiar gravel-in-a-can sound.
Safety Alert: Never loosen a hydraulic hose or fitting on a running machine to search for a leak. Pressurized oil can penetrate skin and cause a medical emergency even when the puncture looks small. Shut down, lower attachments, isolate stored energy, and verify pressure with the approved procedure and equipment.
Confirm Pressure and Flow the Right Way
Pressure testing is useful only when the gauge is installed at the correct test point and rated for the circuit. A deadhead pressure reading can show that the relief valve opens, but it does not prove the pump produces adequate flow. A worn pump can reach near-normal pressure with no load while delivering too little oil for acceptable cycle times.
Measure standby pressure, operating pressure, and flow at a known engine speed. Record oil temperature because hydraulic viscosity changes the result. Compare readings with the manufacturer service information for that exact machine and pump configuration. On electronically controlled equipment, record commanded pump current or control pressure when the system supports it. A pump may be mechanically sound while a sensor, solenoid, wiring fault, or compensator prevents it from receiving the right command.
Hydraulic pump failure analysis should also include case-drain flow when the pump design provides a case-drain port. Excessive case leakage is a strong sign of internal wear. A little leakage is normal; a sudden increase compared with the service limit is not. Catch the oil in a marked container for a timed test, then stop if the procedure requires special adapters or high-pressure connections.
Find the Root Cause Before Installing a Pump
Replacing a pump without finding the cause is how a repair becomes a repeat failure. Inspect the reservoir for sludge, water, and loose coating material. Check the breather, because a restricted breather can create a vacuum in the tank and starve the inlet. Inspect suction hoses for soft spots, collapsed sections, loose clamps, and cracked seals. A hose can look fine from the outside and still pull air through a damaged connection.
Check oil specification and service history. Mixing incompatible fluids, using the wrong viscosity, or extending drain intervals on a dusty site can shorten component life. Confirm that the reservoir level was checked with the machine in the position specified by the manufacturer. An apparently full tank can be dangerously low when cylinders are extended or attachments are raised.
Field Lesson: In Nevada, I found a pump failure caused by a replacement suction hose with a smaller internal diameter than the original. It fit the fittings and looked professional. Under load, it created enough inlet restriction to cavitate the pump. The hose cost less than a hundred dollars; the contaminated pump repair ran into thousands.
Know When the Pump Is Beyond Field Repair
Some work belongs in a clean hydraulic shop. If the pump has seized, shed heavy metal, lost its case, or contaminated the complete system, do not install a remanufactured unit and send the machine back to work. Flush or replace contaminated hoses, filters, valves, and the reservoir as required. Inspect downstream motors and cylinders because debris travels farther than many crews expect.
A qualified shop can measure shaft condition, bearing preload, rotating-group clearances, valve-plate wear, and housing damage. Ask for a written failure report, not just a rebuilt component in a box. The report should identify the failed part, likely cause, test results, and cleaning recommendations. That paperwork protects the next repair and gives the maintenance team a lesson it can use.
Build a Better Maintenance Routine
The most useful hydraulic pump failure analysis happens before the machine stops. Record normal pressure, cycle time, oil temperature, filter condition, and case-drain flow during scheduled inspections. Oil sampling can identify rising particle counts before an operator hears damage. Trend results by machine hours instead of treating each sample as a pass-or-fail event.
Train operators to report changes early: new whining, slower functions, hotter oil, foaming, erratic movement, or a need to raise engine speed for ordinary work. A five-minute report can prevent a full system cleanup. Keep clean caps and plugs in the service truck, use dedicated hydraulic sampling equipment, and never leave an open hose exposed to dust or rain.
My final rule from thirty years in the field is simple: hydraulic pump failure analysis is not about guessing which expensive part to order. It is about separating symptoms from causes, proving the fault with clean measurements, and controlling contamination before it spreads. If pressure, flow, and case-drain tests point to the pump, remove it carefully and document everything. If the evidence points elsewhere, follow it. Stopping for a proper diagnosis beats spending two weeks on a site rebuilding the same failure.