On a copper site outside Calama, Chile, a hydraulic shovel came into the shop sounding like a bucket of bolts. The operator had reported slow swing speed, then a whining pump. We pulled the return filter and found it loaded with bright metal. The oil looked clean in the sight glass. That machine still needed a pump, control valve work, and a production shutdown that cost far more than a proper sample would have. Hydraulic fluid contamination testing would have shown the trouble weeks earlier.
I have seen the same mistake on excavators, wheel loaders, dozers, and underground loaders: somebody judges oil by color and calls it good. Hydraulic oil can look clear while carrying particles small enough to damage a precision spool or an axial piston pump. I've seen this go wrong. Here's how you avoid it.
Why clean-looking oil can still destroy a hydraulic system
Contamination comes in three main forms: solid particles, water, and chemical degradation. Dirt often enters through breathers, open filler caps, damaged seals, dirty service tools, or a replacement hose that was never flushed. A small amount of abrasive dust can score pump plates and wear servo controls. The resulting clearances let even more oil leak internally, so pressure and efficiency fall together.
Water causes a different kind of trouble. Free water can collect in a reservoir, while dissolved water can remain invisible. Either condition can promote rust, reduce lubricating strength, and damage additives. Heat, air entrainment, and oxidation create varnish and sludge that restrict small passages. A filter that plugs repeatedly is not always the root cause; it may be the warning you needed.
The useful question is not simply, “Is the oil dirty?” Ask what contaminant is present, how much is present, and where it entered. Hydraulic fluid contamination testing turns that question into evidence instead of a guess based on a dipstick.
Take the sample correctly or do not trust the report
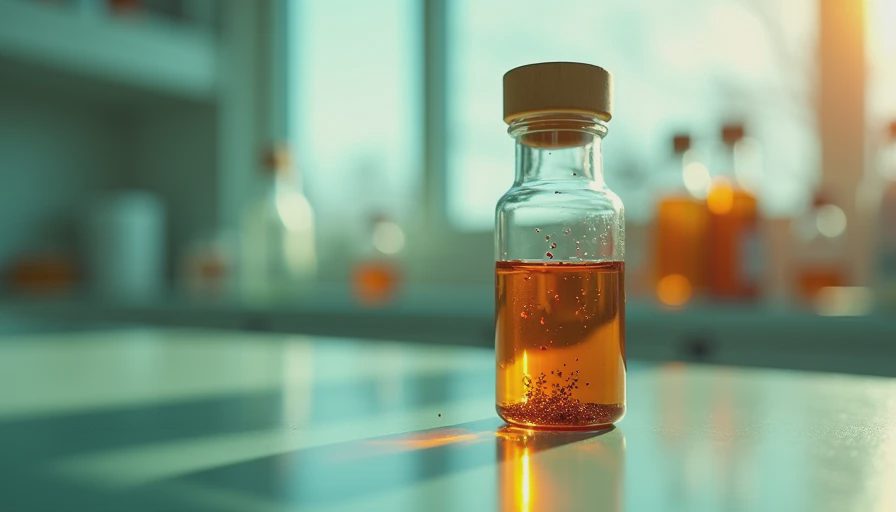
A laboratory cannot repair a bad sample. Sampling from the bottom of a drain pan, a dirty reservoir opening, or an old bottle gives you a story about the sampling process, not necessarily the machine. Use a clean sample bottle supplied by the laboratory. Wipe the port first, flush enough oil to remove stagnant fluid, and collect from a live sampling point while the system is warm and circulating, following the machine maker's procedure.
Never sample immediately after adding new oil unless you are specifically checking the replacement batch. Record the machine model, unit number, engine hours, hydraulic hours if available, oil brand and grade, filter change date, fluid change date, and any recent repairs. A sample without operating context is much harder to interpret.
For a large excavator, I prefer a permanent sampling port in the return line or pressure-side diagnostic circuit when the manufacturer provides one. Do not loosen a high-pressure fitting to collect oil. Hydraulic injection injuries can require emergency surgery and amputation. Shut the machine down, relieve stored pressure, and use the approved port. Safety Alert: a pinhole leak can penetrate skin even when it looks like a harmless mist.
What a useful laboratory report tells you
A strong report usually includes particle count, elemental analysis, viscosity, water measurement, and an assessment of oil condition. Particle count reports often use ISO cleanliness codes. The code does not tell you whether oil is acceptable by itself; compare it with the equipment manufacturer's target and your historical trend. A mining shovel, a compact skid steer, and a servo-controlled press do not necessarily need the same cleanliness level.
Elemental analysis can identify iron, copper, chromium, silicon, aluminum, and other wear or ingression markers. High silicon can point toward dirt entry, though it must be interpreted with the full report. Rising copper may indicate bushing or cooler-related wear. A viscosity change can indicate the wrong fluid, shear, oxidation, or contamination with another product. Karl Fischer testing or a comparable laboratory method can quantify water more reliably than visual inspection.
Hydraulic fluid contamination testing is most valuable as a trend. One abnormal result deserves attention; repeated results show direction. A gradual rise in iron followed by increasing particle counts often tells you a component is wearing before performance drops enough for an operator to notice.
Reading the warning signs in the field
Suppose a wheel loader sample shows a cleanliness code moving from the fleet's normal range to a visibly dirtier level, with silicon rising and viscosity still normal. That pattern points first toward external dirt ingress: a torn breather, loose filler cap, poor service practice, or a seal problem. Inspect those paths before condemning the pump. Change the filter using the correct rating, clean the reservoir area, repair the entry point, and resample after a controlled operating interval.
Now consider an excavator with elevated copper and iron, falling efficiency, and a complaint of sluggish functions when hot. That combination deserves a system inspection, not just an oil change. Check pump case drain flow, standby pressure, pilot pressure, cooler performance, and control valve behavior with the machine's service specifications. Do not keep running it until the pump fails completely; debris from one damaged component can circulate through the rest of the system.
Field Lesson: on a western U.S. quarry loader, a recurring dirty sample led us toward the return filter. The real cause was a replacement breather installed without its protective cap during servicing. The fix cost minutes. The earlier habit of changing filters without finding the entry path had cost several filters and a great deal of confusion.
Build a practical sampling program
Start with a baseline sample after a known-good fluid and filter change. Sample at a consistent interval, such as every 250 operating hours for equipment working in severe dust, or according to the manufacturer's maintenance schedule. High-hour mining equipment may justify more frequent monitoring. Keep the interval consistent so changes mean something.
Use a simple spreadsheet or maintenance system with one line per machine. Track sample date, hours, oil type, particle count, water, viscosity, wear metals, filter changes, repairs, and laboratory comments. Mark results as normal, watch, or action required. A single red result should trigger verification and inspection, not an automatic component replacement. Confirm the sample identity and consider resampling when the result conflicts with machine behavior.
When hydraulic fluid contamination testing shows a sharp change, quarantine questionable service materials and inspect the reservoir, breathers, hose interiors, cylinder rods, filter elements, and cooler. Flush procedures vary by machine and contamination type. A basic drain-and-fill may not remove debris trapped in lines, valves, or cylinders. Severe metal contamination can require component cleaning, filter replacement, flushing, and a follow-up sample.
When the smart move is to stop the machine
Stop and call a qualified hydraulic shop when you find visible metal, milky oil, repeated filter collapse, sudden loss of pressure, uncontrolled movement, or a rapidly worsening lab trend. Keep people clear of suspended loads and isolate stored hydraulic energy before inspection. A clean sample is useful, but it does not make an unsafe machine safe.
The cheapest repair is usually the one made while the problem is still a contaminated sample and not a failed pump. Hydraulic fluid contamination testing gives a foreman time to plan parts, schedule a bay, and protect production instead of waiting for a machine to quit in the worst possible place.
My rule after three decades in the field is straightforward: sample consistently, document everything, and investigate the entry path. Do not let clear oil fool you. If the report is worsening, believe the trend before the machine makes the decision for you.