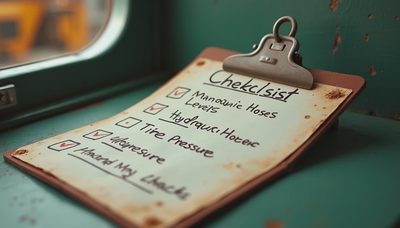
At a copper operation outside Antofagasta, I watched a haul truck limp into the shop with a final drive hot enough to blister paint. The operator had reported a small oil seep three shifts earlier. Nobody stopped the truck. By the time we opened the drain, the gear oil looked like metallic soup, and the repair bill had moved from a seal job to a full planetary rebuild. That is the hard lesson behind fleet maintenance cost reduction: the cheapest repair is usually the one you catch before the machine announces it with smoke, heat, or a locked-up component.
I spent 30 years chasing failures on Caterpillar machines across mines, quarries, road projects, and heavy construction sites. Here is what worked in the real world, where rain, dust, production pressure, and tired crews test every maintenance plan.
Start With Failure Prevention, Not a Bigger Parts Discount
Fleet maintenance cost reduction begins with knowing which failures can stop production. A torn loader bucket corner is inconvenient. A low engine oil warning ignored on a D8 dozer can destroy an engine. Rank your equipment by replacement cost, production value, safety exposure, and failure history. Put the best inspection discipline on the machines that can create the largest operational and financial mess.
Build a short list of critical systems for each model: engine oil and coolant, hydraulic oil, transmission, final drives, brakes, steering, tires, and undercarriage. Give operators a simple walkaround sheet with specific checks instead of vague instructions such as “inspect machine.” Ask for visible leaks, unusual noise, warning lights, hot smells, loose guards, damaged hoses, and changes in track or tire behavior.
A ten-minute walkaround can expose a loose hose clamp or cracked fitting before it empties a hydraulic tank. It cannot replace a qualified technician, but it gives that technician an earlier starting point. Record the defect, machine hours, location, and urgency. A notebook in the cab is better than memory, while a shared digital log makes trend tracking easier across a large fleet.
Make Fluid and Filter Control a Shop Discipline
I have seen more expensive iron damaged by contamination than by hard work. A hydraulic pump does not care whether the dirt entered through a dirty funnel or a careless bulk tank. It will still charge you for the mistake. Fleet maintenance cost reduction depends on clean fluids, correct filters, and disciplined sampling.
Store drums under cover, off the ground, and with caps closed. Mark hydraulic oil, engine oil, transmission fluid, and coolant clearly. Do not use a cut-off plastic bottle as a measuring container. Use clean transfer pumps and dedicate them to the right fluid. A few hundred dollars spent on proper handling equipment is cheap compared with a contaminated pump, valve bank, or injector system.
Oil sampling is useful when someone acts on the results. A rising iron reading, coolant trace, fuel dilution, or abnormal silicon level should trigger a planned inspection. It is not a magic prediction machine, and a sample does not give permission to keep running a machine with low pressure, severe noise, or overheating. Stop unsafe equipment first, then diagnose it correctly.
Filters deserve the same attention. Use the specification approved for the machine and inspect the old filter when practical. Pleats packed with fine dust, shiny metal, rubber fragments, or coolant residue can tell a better story than a generic service note. Change intervals should reflect the environment. A loader working in dry silica dust may need more frequent air filter attention than the same model loading clean aggregate indoors.
Schedule Work Around Production Instead of Waiting for Failure
Unplanned downtime is expensive because it brings secondary costs: a replacement machine, idle operators, expedited freight, lost haulage, and a crew standing around. Planned maintenance still costs labor and parts, but it lets the foreman choose the time, technician, tooling, and repair scope. That is the center of fleet maintenance cost reduction for most contractors.
Use engine hours, not calendar dates alone. A skid steer that runs 400 hours each month needs a different service rhythm from a backup excavator that runs 40. Set service windows before major production milestones, such as a road pour, overburden push, or seasonal mine shutdown. Combine inspections while the machine is already down. Checking belts, battery connections, hose routing, grease lines, and cooling-pack condition during an oil service takes less time than arranging separate stoppages.
Do not stretch a service interval just to make a weekly utilization report look good. If a machine is operating in mud, extreme heat, high altitude, or abrasive dust, the maintenance plan must reflect those conditions. I have shortened intervals in the field when the evidence justified it, then restored them after clean sampling and inspection showed the machine was stable.
Control Parts Without Stocking a Museum
A parts room can quietly consume cash. I have walked into shops carrying three brands of the same common filter, obsolete seals for retired machines, and expensive components nobody could identify. Fleet maintenance cost reduction does not mean buying the cheapest part. It means holding the right parts, at the right quantity, with enough information to prevent wrong orders.
Create a critical-spares list for each machine group. Common filters, belts, hose fittings, O-rings, electrical relays, grease, fluids, and service kits usually deserve predictable stock. Large components such as hydraulic pumps, turbochargers, and final-drive assemblies need a different decision based on lead time, fleet size, failure history, and whether a rental or dealer exchange is realistically available.
Track part numbers, supersessions, shelf life, storage location, and issue history. Rotate rubber products and fluids properly. Before ordering, verify the serial-number range and machine configuration. Two excavators with the same model badge can have different pumps, harnesses, or control valves because of a production change. The ten minutes spent confirming fitment beats an overnight freight charge and another day of downtime.
Use Operators as Your First Diagnostic Instrument
The operator often knows a machine is changing before a scan tool does. A new vibration while swinging an excavator, a loader transmission that hesitates when hot, or a haul truck retarder that feels different should be treated as useful evidence. Do not punish operators for reporting small symptoms. If every report gets dismissed as “normal wear,” the crew learns to stay quiet until something breaks.
Hold short defect reviews at the start of a shift. Ask what changed, when it started, under what load, and whether the problem is constant or intermittent. A good description can save hours of fishing. Write “hydraulic function slows after 20 minutes at operating temperature,” not “hydraulics bad.” The first statement points a technician toward heat, oil condition, relief settings, or pump efficiency.
Safety Alert: no operator or technician should inspect beneath raised equipment, enter a pinch point, or work near an energized attachment without the proper lockout, blocking, and site procedures. A maintenance saving is worthless if someone gets crushed. Shut down, isolate energy, lower attachments where possible, and use rated stands or blocking. Never trust hydraulic pressure to hold a machine up.
Measure the Program by Repair Decisions
Fleet maintenance cost reduction becomes real when the shop can explain why a repair was made and whether it prevented a larger loss. Track downtime hours, repeat defects, emergency freight, warranty recovery, planned versus unplanned work, and component life. You do not need a complicated software package to begin. A clear spreadsheet connected to machine hours can reveal which model, system, or work practice is consuming money.
Review the numbers monthly with the foreman, lead technician, and operations supervisor. If one wheel loader repeatedly destroys cutting edges, inspect operator technique, material conditions, bucket selection, and tire pressure before blaming the parts supplier. If the same electrical connector fails after every wash, change the routing or protection instead of repeatedly replacing the connector.
Field Lesson: on a western road project, we reduced repeated cooling problems by cleaning the radiator pack properly and correcting daily inspection habits. The fix was not a more expensive radiator. It was removing packed dust before the machine overheated. That is how fleet maintenance cost reduction should look: fewer surprises, better decisions, and no shortcuts around safety.
I've seen this go wrong. Here's how you avoid it: inspect early, keep fluids clean, plan the work, stock intelligently, listen to operators, and stop unsafe equipment. When a failure involves brakes, steering, structural damage, high-pressure hydraulics, or a major powertrain, call a qualified heavy-equipment shop. Production can wait. A person cannot be replaced.